Binhnam Aluminium operates a 50,000 m² manufacturing facility with 6 extrusion lines and integrated aluminium production capability. From billet preparation and extrusion to surface finishing, CNC machining and quality inspection, we control key production steps to support stable quality and efficient delivery.
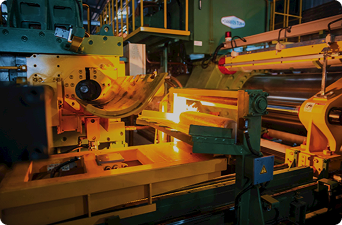
Binhnam Aluminium operates 6 aluminium extrusion lines for producing industrial profiles, construction profiles and custom aluminium extrusion products. Our extrusion capability supports different profile shapes, product structures and application requirements based on customer drawings or standard product specifications.
Binhnam Aluminium provides aluminium surface finishing solutions to improve product appearance, durability and corrosion resistance. Our surface finishing options include powder coating, anodizing and wood grain finishing, with color and finish requirements customized according to project needs.
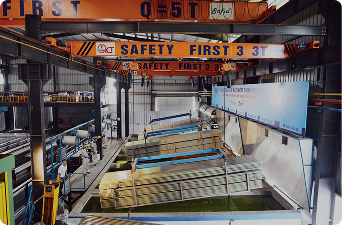
For customers who need further processing after extrusion, Binhnam Aluminium provides CNC machining and fabrication support. CNC machining helps customers receive aluminium profiles that are closer to final assembly requirements, reducing additional processing work after delivery.
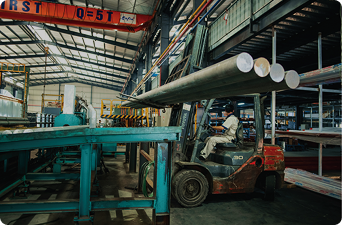
Quality control is applied throughout the aluminium manufacturing process, from raw material inspection to extrusion, surface finishing, machining, packing and final delivery. Our QC process helps ensure product consistency, dimensional accuracy, surface quality and packaging reliability before shipment.
Binhnam Aluminium supports B2B customers through a clear and practical order handling process. Whether you need standard aluminium profiles or a new custom extrusion project, our team helps review your requirements and provide a suitable production solution.

Customers send drawings, samples, product photos or technical requirements to Binhnam Aluminium. Our team reviews the basic information, including product type, application, alloy requirements, surface finish, estimated quantity and delivery expectations.

Our technical team evaluates the profile design, extrusion feasibility, surface finishing requirements, machining needs and packaging method. For custom aluminium profiles, we may suggest adjustments to improve extrusion stability, production efficiency or final product performance.

After reviewing the requirements, Binhnam Aluminium provides quotation details, including product cost, die cost if applicable, MOQ, estimated lead time and production process. The production plan can be adjusted based on order quantity, technical complexity and delivery schedule.

For new custom profiles, we proceed with die development after confirmation. Trial extrusion is carried out to produce samples for inspection and customer approval. The sample stage helps confirm profile dimensions, structure, surface quality and application suitability before mass production.

After sample approval, Binhnam Aluminium begins mass production according to the confirmed specifications. Quality control is carried out during extrusion, surface finishing, CNC machining and final inspection to ensure product consistency before shipment.

Finished aluminium profiles are packed according to product type, surface finish and export requirements. Our team prepares the necessary documents and supports delivery based on the agreed shipping terms.
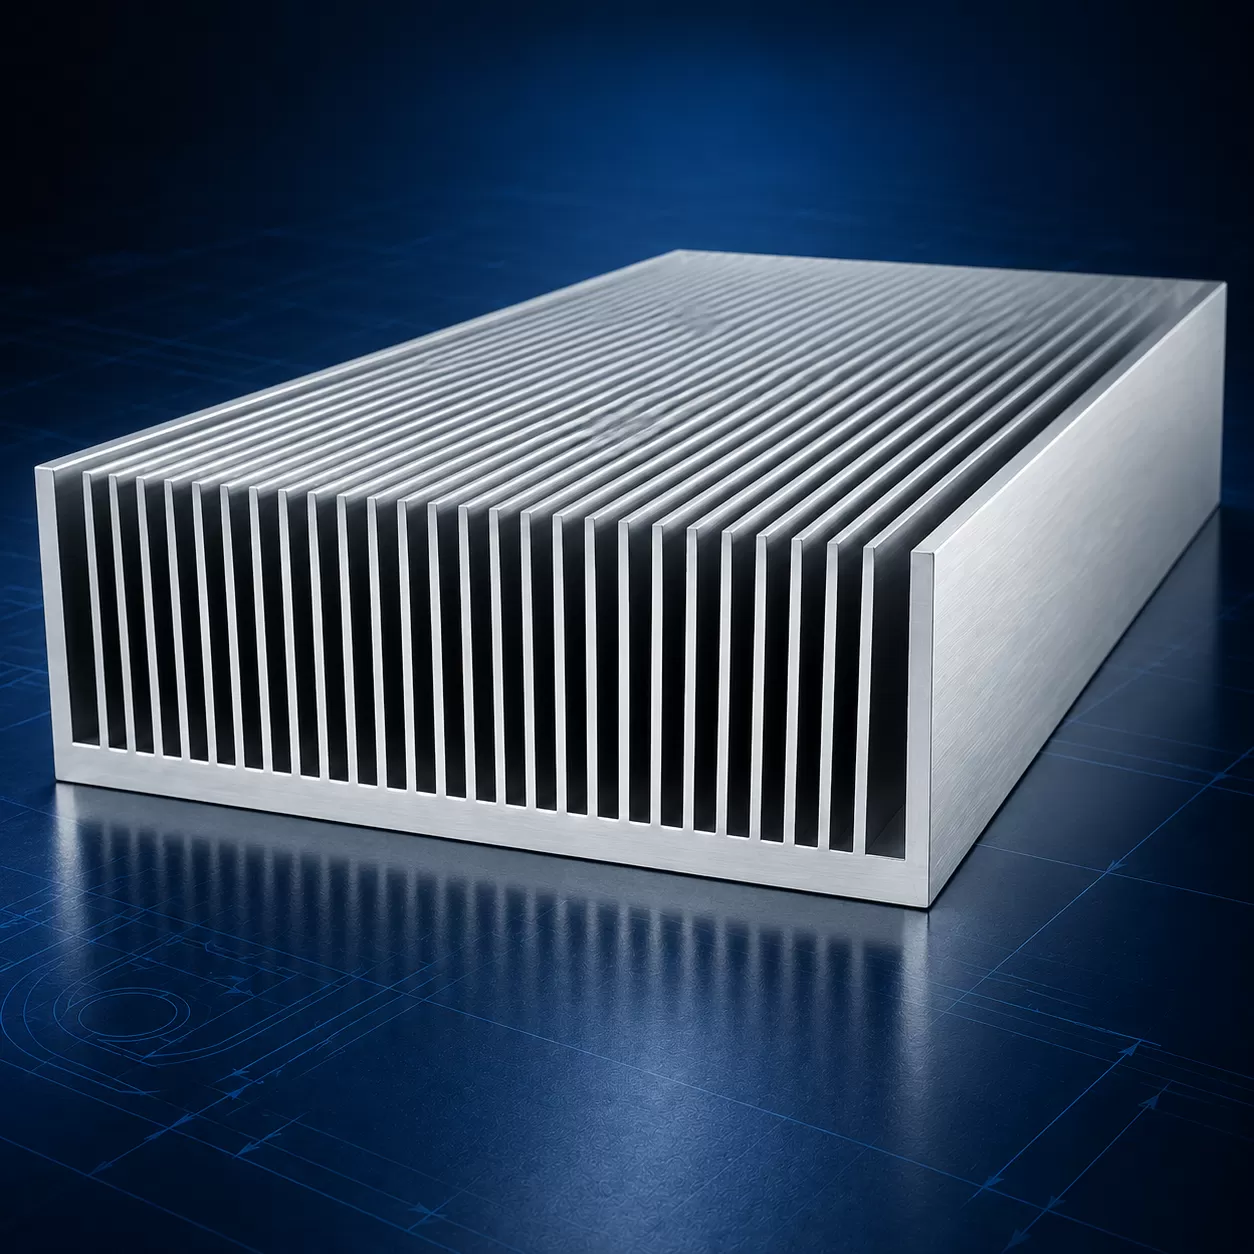
Extruded aluminium heat sink profiles for power electronics, inverters, power supplies and industrial control equipment. Binhnam Aluminium supports existing-tooling review and custom manufacturing based on customer drawings and application requirements.
Power aluminium heat sink profiles are extruded aluminium components designed to help transfer heat away from power electronic devices and other heat-generating electrical components.
Typical applications include power supplies, inverters, converters, industrial control equipment and other electronic systems where thermal management forms part of the product design.
A power heat sink typically combines a mounting base with fins or other heat-dissipating surfaces. Depending on the equipment, the extrusion may also incorporate structural walls, mounting grooves, enclosure features or interfaces required for assembly.
Unlike a general aluminium profile, heat sink selection should consider both manufacturing geometry and the complete thermal system. Important factors may include the heat source, contact surface, fin configuration, available airflow, installation space and operating environment.
Binhnam Aluminium can review existing extrusion tooling or develop custom power heat sink profiles according to approved drawings, physical samples and technical requirements.
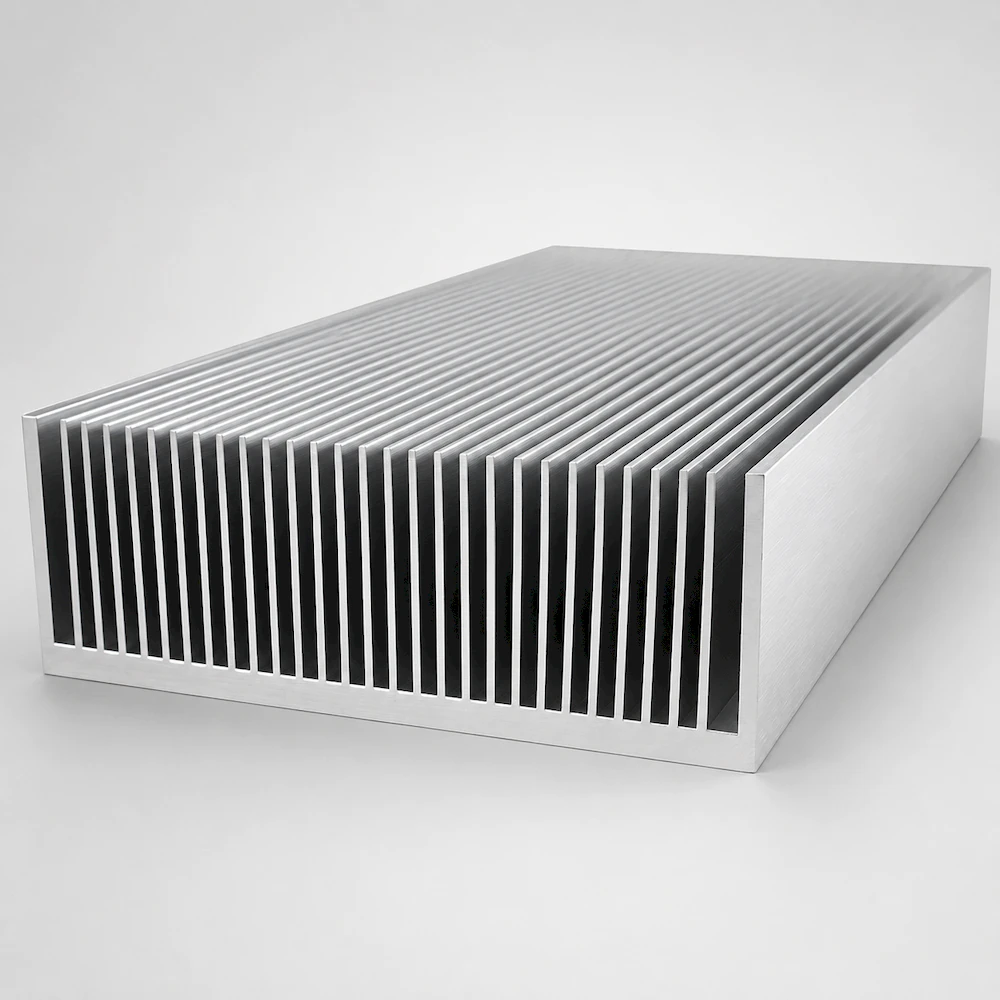
Dense-fin heat sinks incorporate multiple closely arranged fins to increase the available aluminium surface area within a compact profile.
They can be considered for power electronic equipment where the approved thermal design requires a relatively large heat-dissipating surface within limited installation space.
Fin height, thickness, spacing and base geometry should be reviewed together because increasing fin density does not automatically improve thermal performance under every airflow condition.
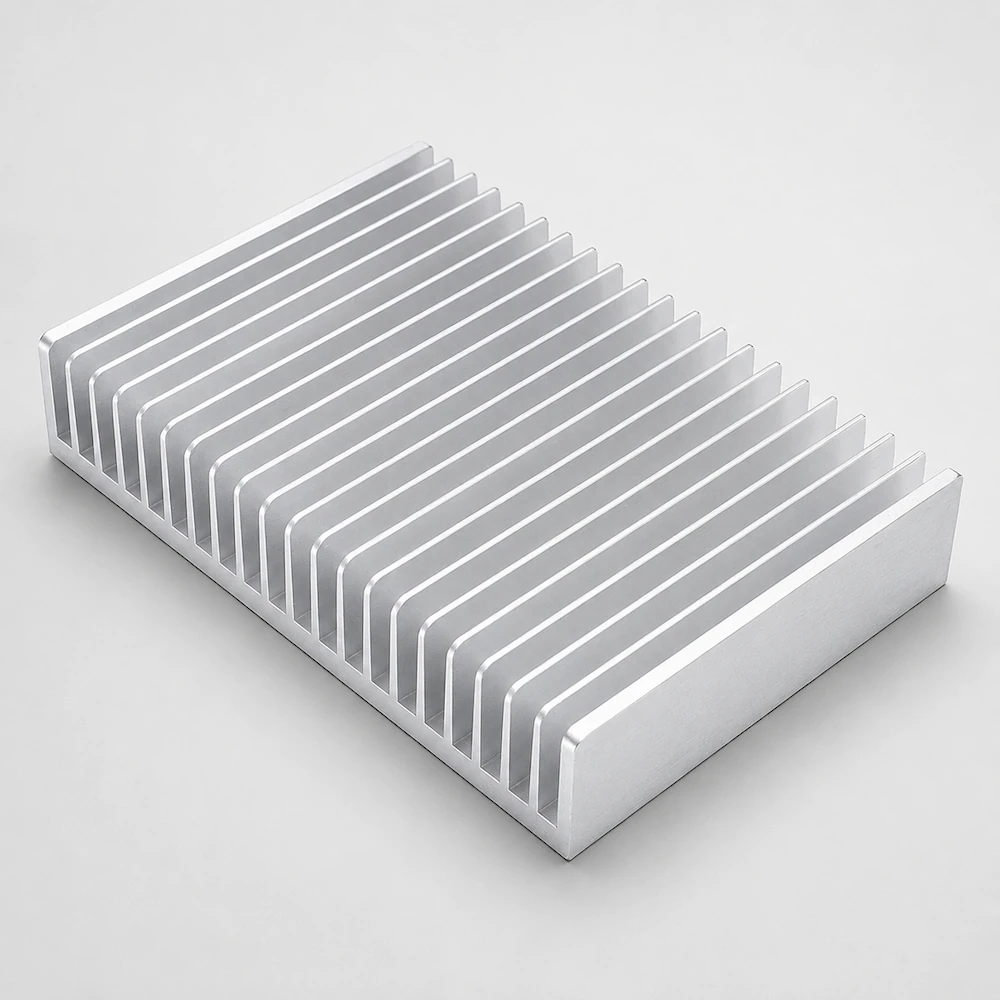
Plate-fin heat sinks use parallel fin structures extending from a flat aluminium base.
This configuration provides a straightforward mounting surface for power components while the fins provide additional surface area for transferring heat to the surrounding environment.
Plate-fin profiles can be considered for power supplies, electronic assemblies and industrial electrical equipment, subject to the actual thermal and mechanical requirements.
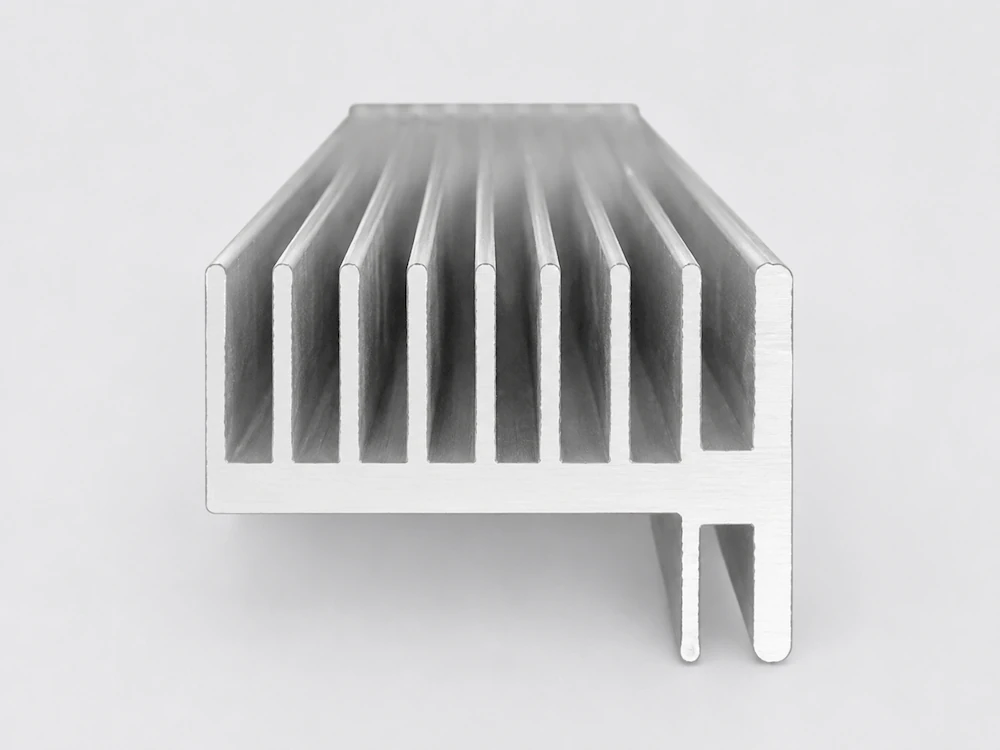
Wide-base power heat sinks provide an enlarged mounting area for applications involving larger power modules or multiple heat-generating components.
The cross-section may combine a broad contact surface with external fins to support both component mounting and heat dissipation.
These profiles can be considered for inverters, converters and other power electronic assemblies where the base geometry must accommodate the equipment layout.
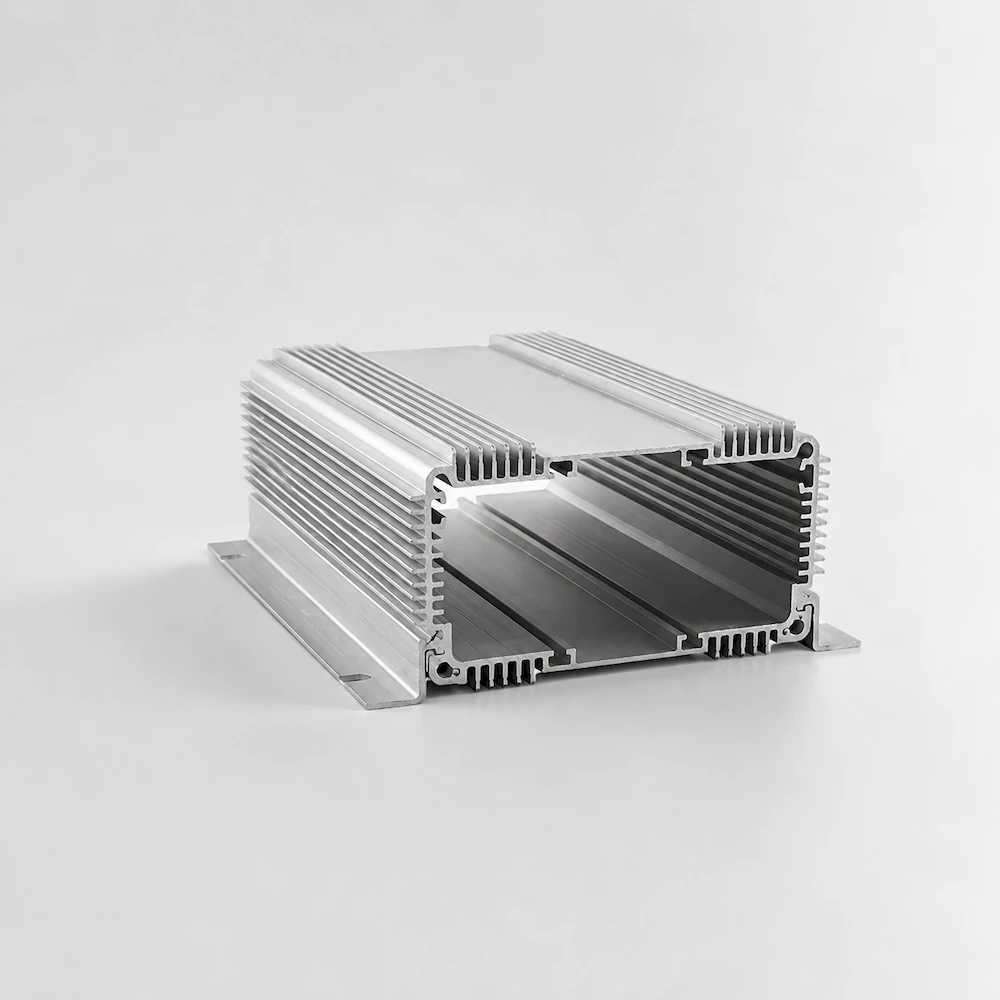
Heat sink enclosure profiles combine heat-dissipating surfaces with structural housing functions within a single aluminium extrusion.
Depending on the approved cross-section, the profile may include external fins, internal mounting surfaces, walls, grooves and interfaces required for the electrical assembly.
These configurations can be considered where the aluminium housing itself forms part of the thermal-management system.
Final specifications are confirmed according to the approved drawing, thermal application and manufacturing requirements.
| Item | Specification |
|---|---|
| Product Name | Power Aluminium Heat Sink Profiles |
| Product Type | Extruded aluminium heat sink for power electronics and industrial electrical equipment |
| Material | Aluminium alloys including 6005, 6005A, 6082, 6060, 6061, 6063, 7005, 3003 and 5052 at factory level, subject to profile design, extrusion feasibility and application requirements |
| Temper | T5, T6 or other applicable tempers, subject to selected alloy, required mechanical properties and project specifications. Final alloy–temper combinations are confirmed during technical review |
| Profile Design | Existing-tooling or custom power heat sink extrusion |
| Base Geometry | Mounting base dimensions and wall configuration according to the approved drawing |
| Fin Geometry | Fin height, thickness, spacing and arrangement are project-specific |
| Mounting Interface | Contact surfaces, grooves and mounting features according to application requirements |
| Surface Finish | Mill Finish, Anodizing, Powder Coating, Metallic Coating, Wood-Grain Finish or approved Custom Finish, subject to thermal and product suitability review |
| Processing | Cutting and project-based drilling, tapping, milling, holes or slots |
| Length | Custom length subject to profile geometry, finishing, machining, packing and transport review |
| Applications | Inverters, power supplies, converters, industrial controls, electronic equipment and OEM power systems |
| Packaging | Selected according to fin geometry, finished surfaces and shipping requirements |
Binhnam Aluminium's confirmed factory-level alloy capability includes 6005, 6005A, 6082, 6060, 6061, 6063, 7005, 3003 and 5052; however, these grades should not be treated as automatically suitable for every heat sink design.
Important Thermal Design Considerations:
Heat sink performance depends on the complete thermal system rather than the aluminium extrusion alone.
Important factors can include:
For this reason, Binhnam Aluminium should not publish one universal thermal resistance or heat-dissipation rating for the entire category. Where thermal performance must meet a specific target, buyers should provide the applicable design requirements or validation method during technical review.
Fins and other external aluminium surfaces can increase the area available for heat transfer from the power component to the surrounding environment.
The actual thermal benefit depends on the fin configuration and operating conditions.
Power heat sinks can incorporate a flat or application-specific base for installing power modules, electronic components or associated assemblies.
Critical mounting areas should be identified on the technical drawing.
Fin height, thickness, spacing and arrangement can be developed according to the approved profile design and extrusion feasibility.
This enables the extrusion to be adapted to different equipment layouts and thermal systems.
Depending on the cross-section, the heat sink may also perform structural or enclosure functions within the equipment.
Grooves, mounting faces and other interfaces may be integrated into suitable custom extrusions.
Binhnam Aluminium can review project-based cutting and CNC operations for power heat sink profiles.
Processing may include drilling, tapping, milling, holes and slots according to the approved fabrication drawing.
Heat sink profiles can be supplied with different finishes according to appearance, environment and product requirements.
For thermal applications, critical contact surfaces and coating placement should always be considered during technical review.
Surface finish should be selected according to appearance, application environment, downstream processing and thermal requirements.
For power heat sinks, finishes applied to thermal-contact areas require particular attention because not every coating should automatically cover every surface.
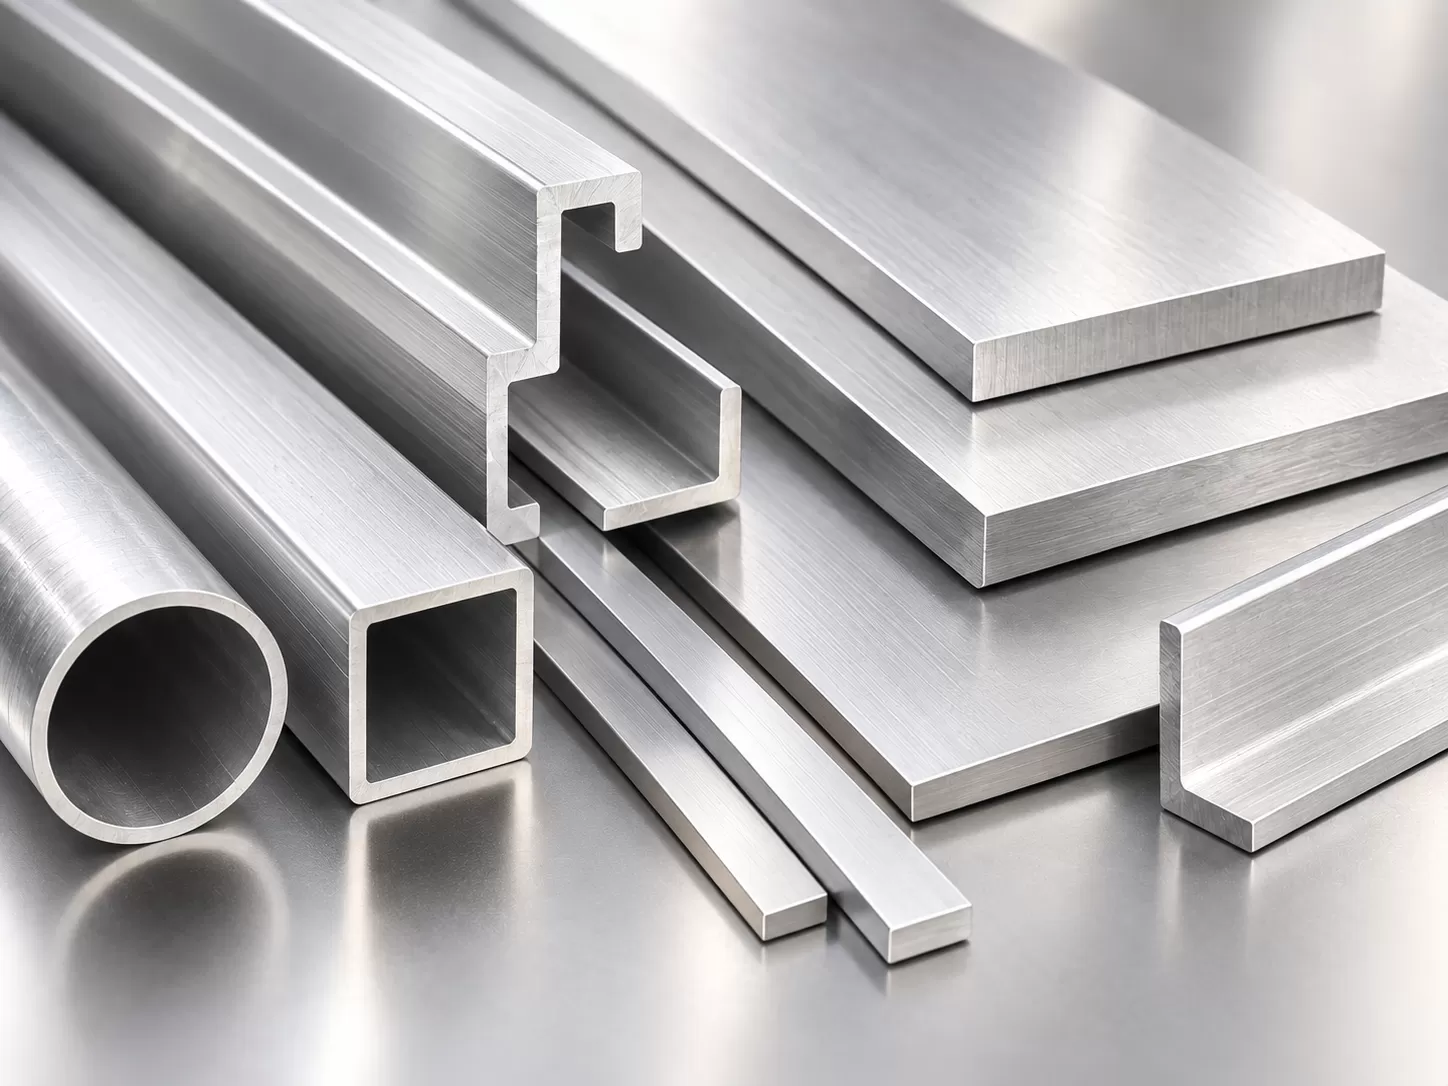
Mill finish is suitable for general heat sink extrusion, further machining and applications where no additional surface coating is required.
It can also simplify subsequent machining of mounting and contact surfaces.
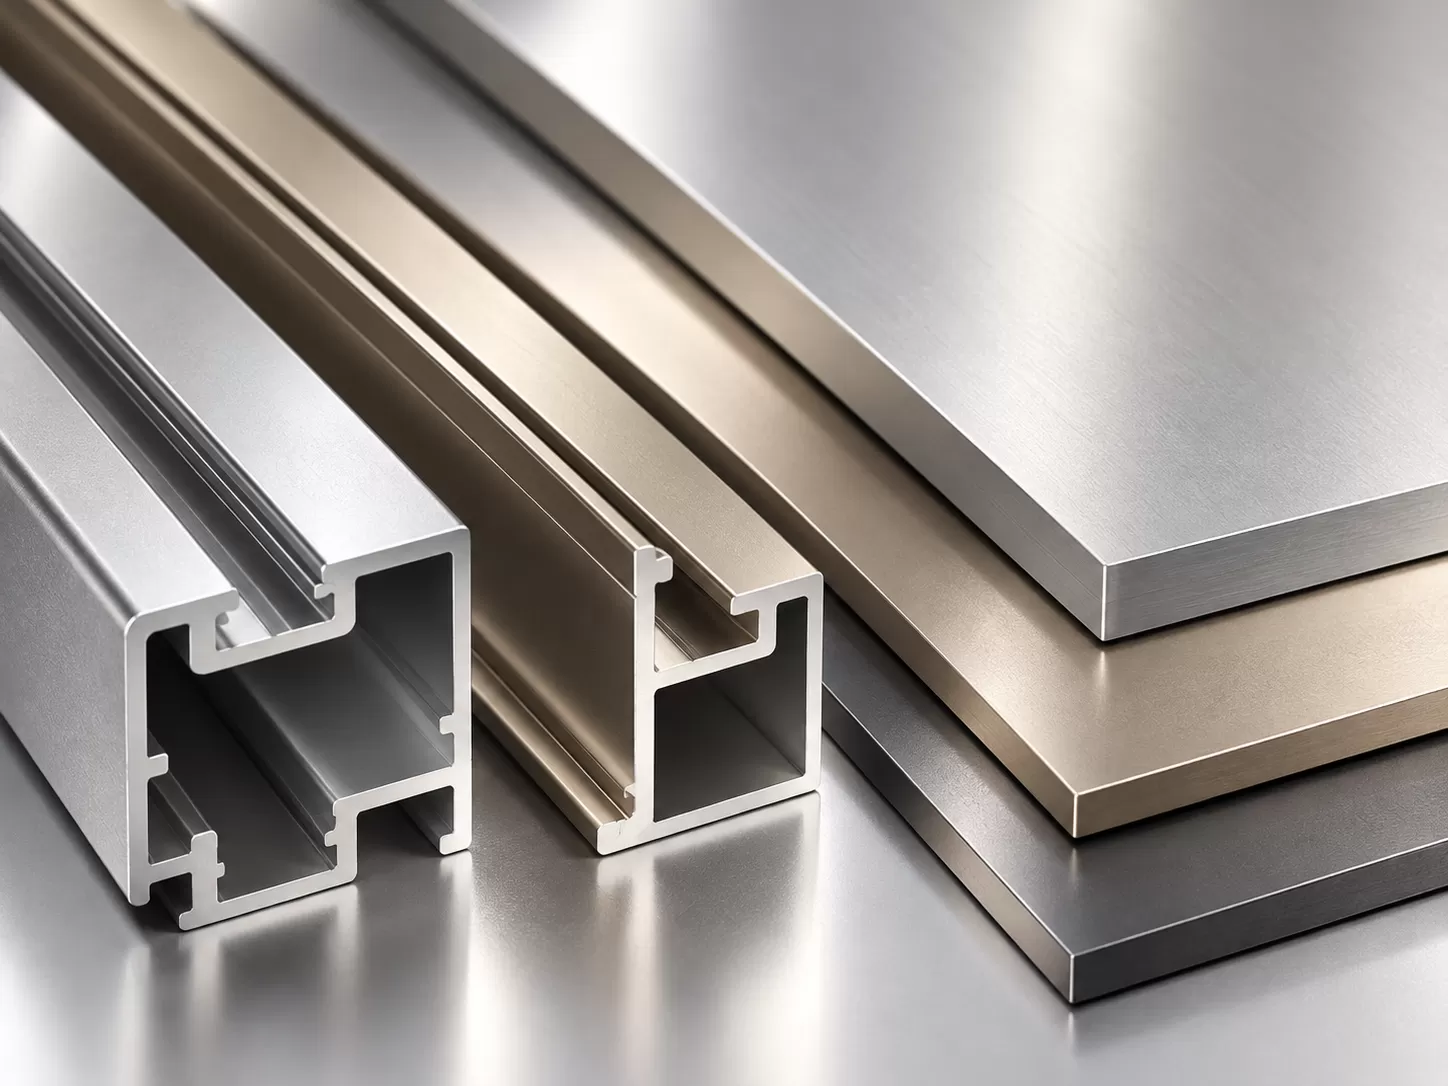
Binhnam Aluminium operates anodizing capability for suitable aluminium profiles.
Anodizing requirements should be reviewed together with alloy selection, thermal-contact surfaces and the intended operating environment.
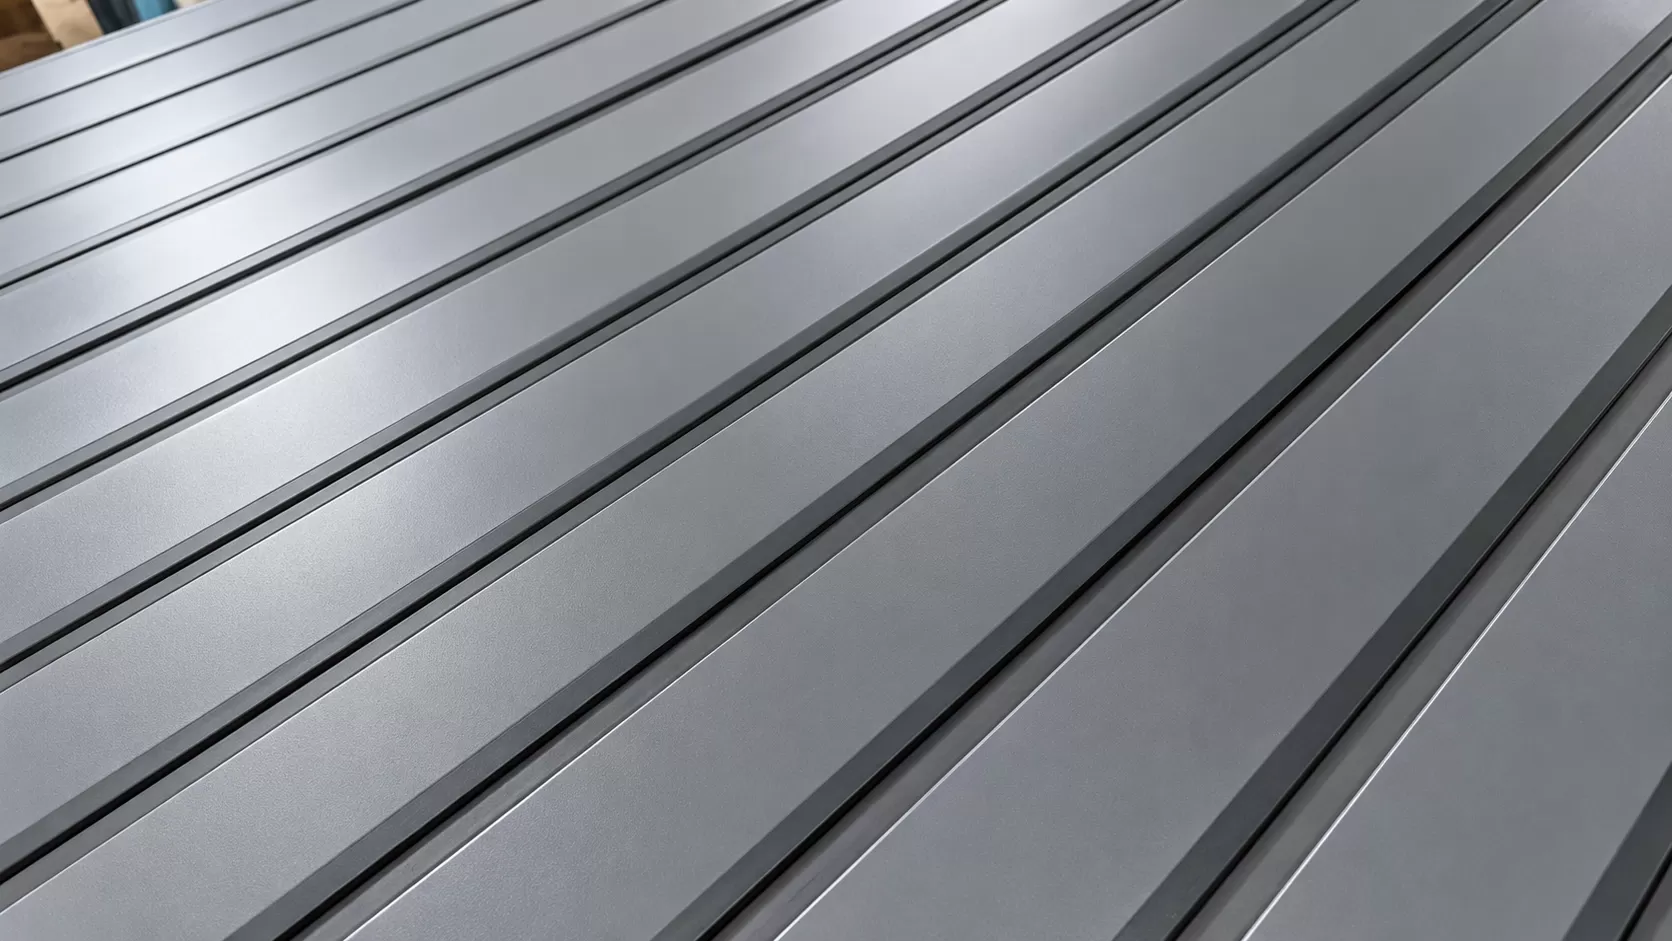
The factory operates a vertical powder-coating line.
Powder coating may be considered for enclosure-integrated heat sinks or visible housing surfaces where the coating is compatible with the approved thermal design.
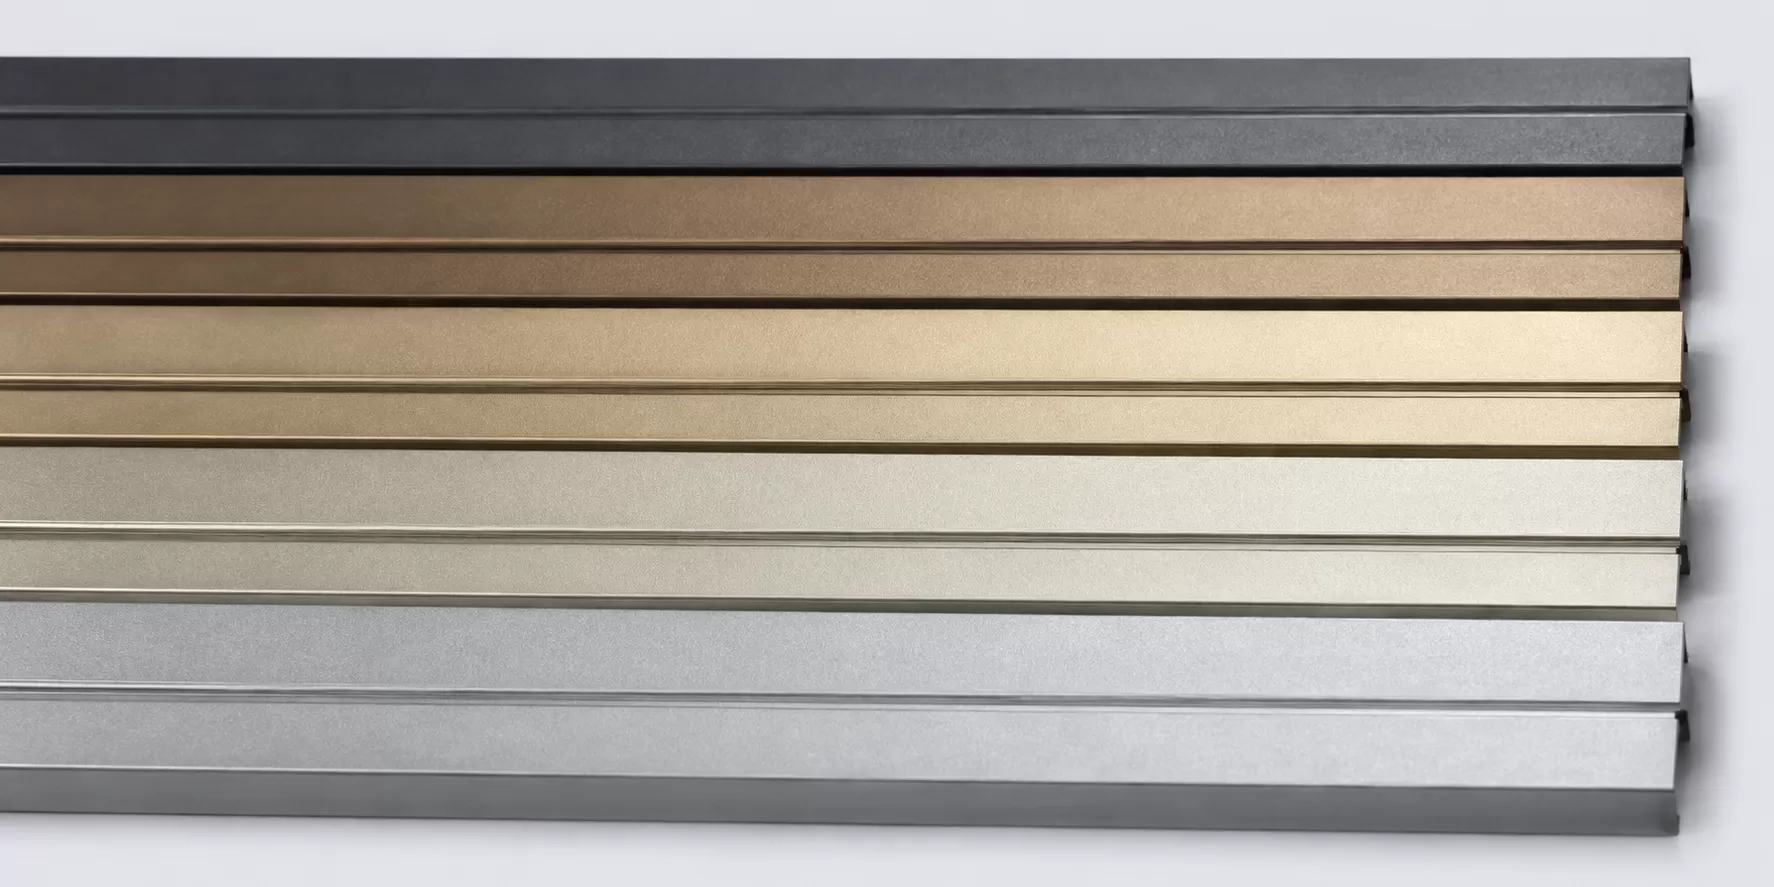
Metallic coating can be reviewed where the visible aluminium component requires a metallic-effect appearance.
For the website, this should be understood as a project-specific metallic-effect finish rather than treated as a separate confirmed coating production line.
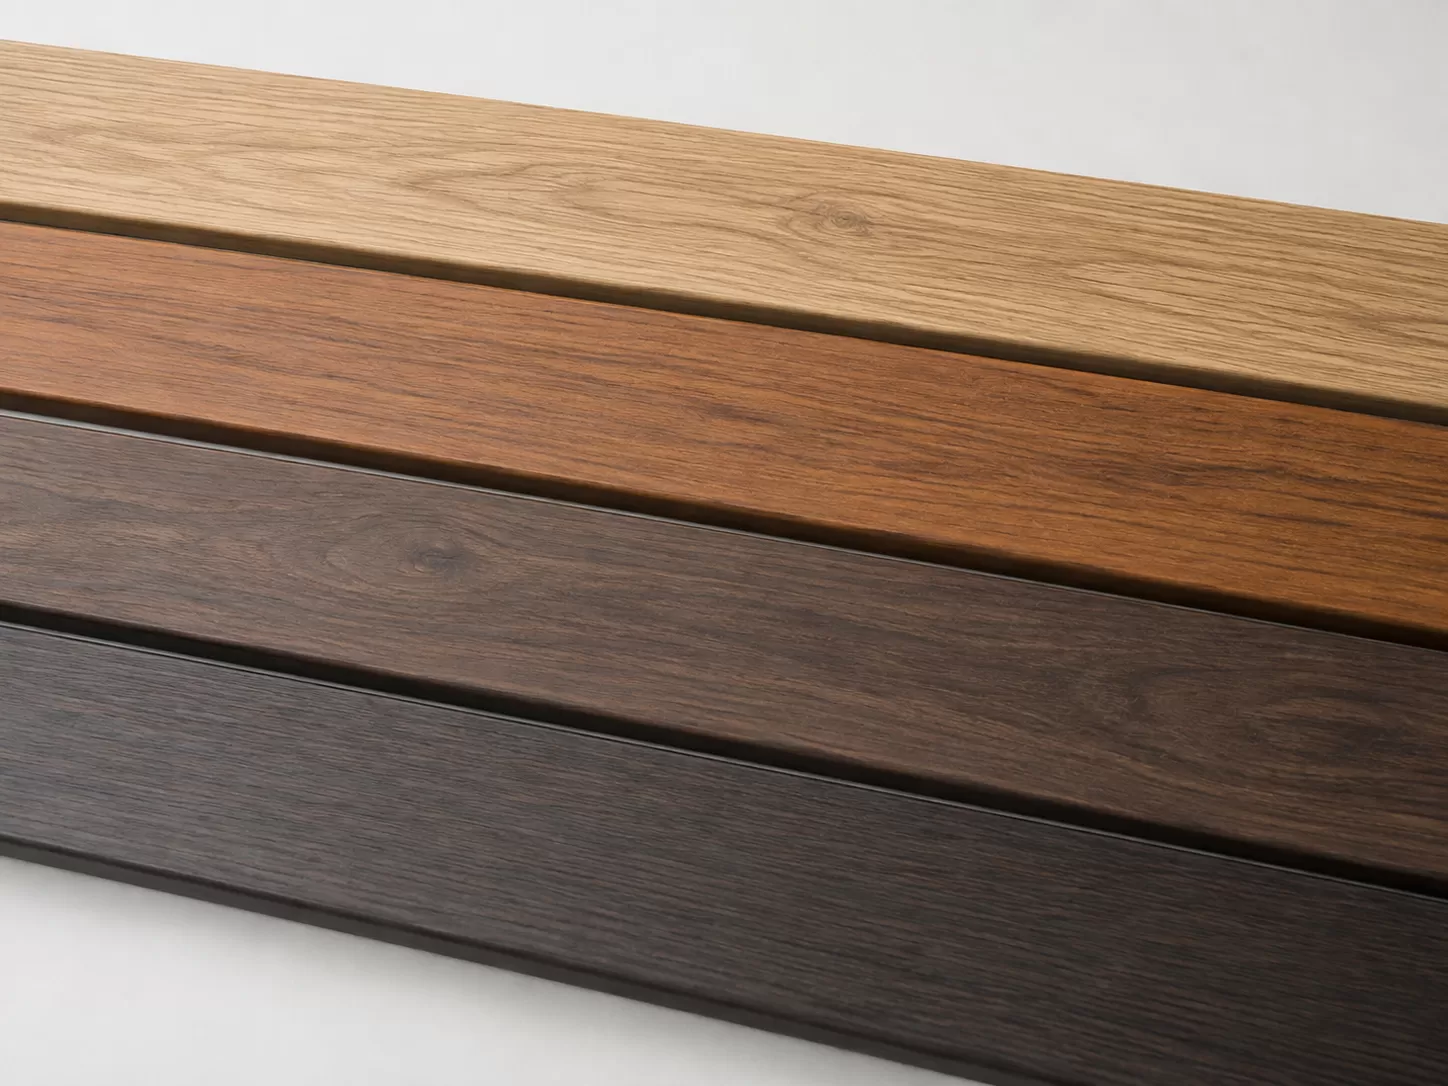
Wood-grain finishing is generally appearance-oriented rather than thermal-performance-oriented.
It may be reviewed for specialised enclosure applications where the decorative finish is compatible with the complete product design.
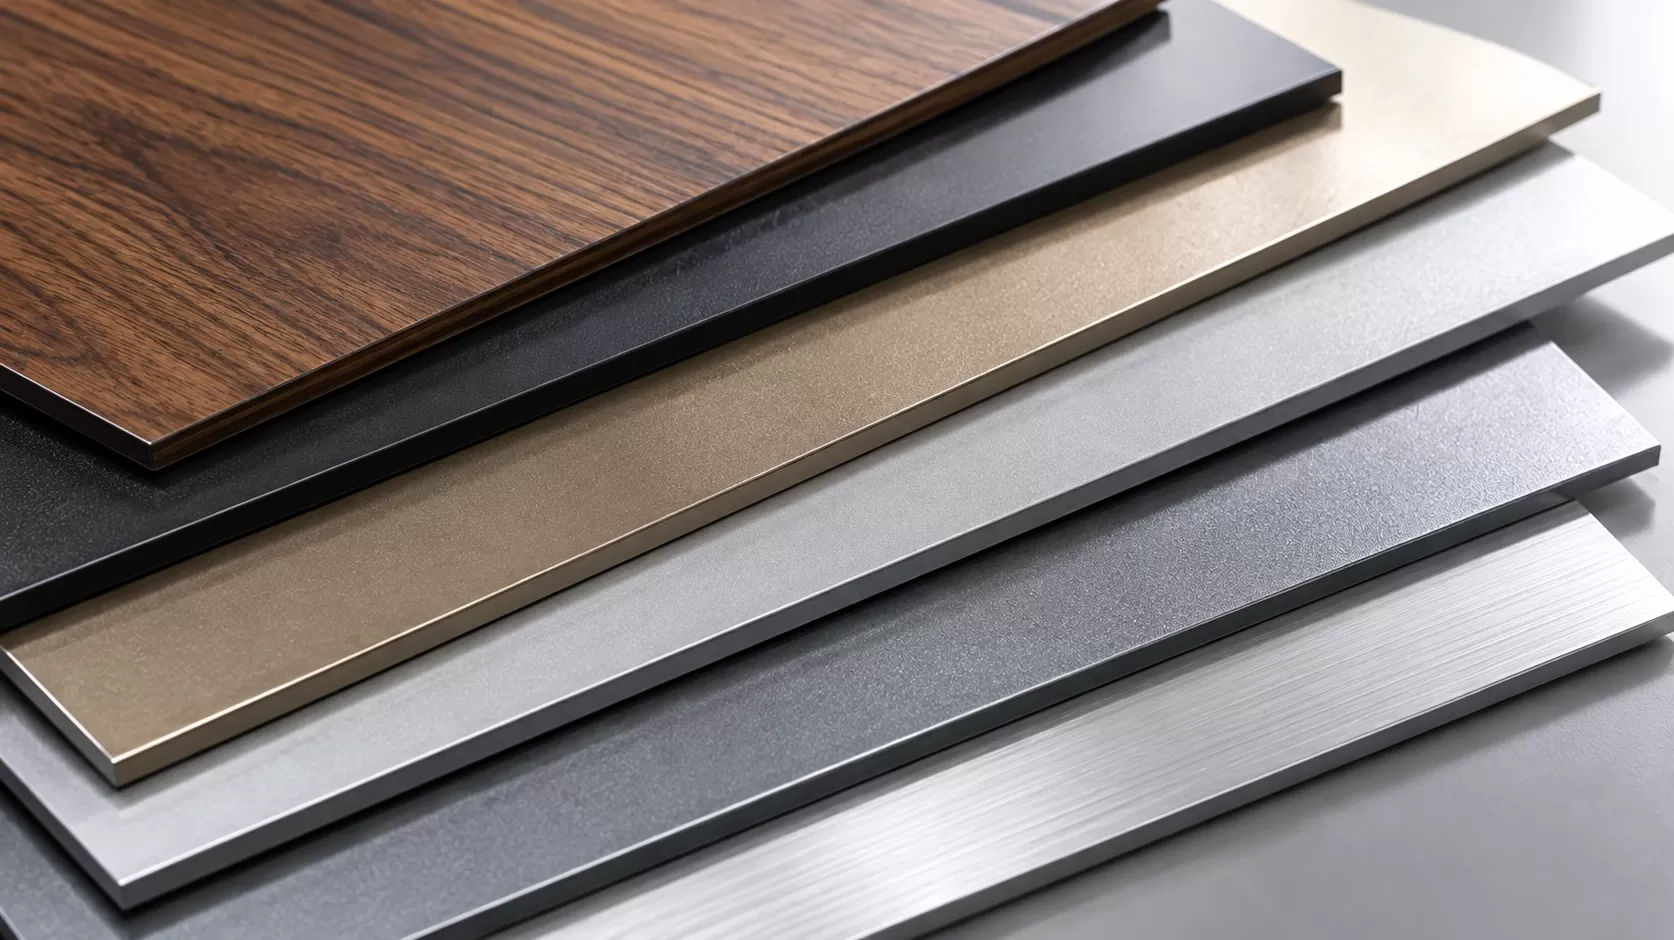
Project-specific colour or appearance requirements can be reviewed according to the profile design, alloy, operating environment and approved specification.
A power aluminium heat sink is a heat-dissipating component used with power electronics and other heat-generating electrical equipment.
It generally includes a component-mounting base together with fins or other surfaces that help transfer heat to the surrounding environment.
Yes, subject to extrusion feasibility.
Fin height, thickness, spacing and arrangement can be specified according to the approved heat sink drawing.
Yes.
Drilling, tapping, milling, holes and slots can be reviewed as project-based CNC operations according to an approved drawing.
No universal thermal resistance value should be applied to the whole category.
Thermal performance depends on profile geometry, component mounting, thermal interface, airflow and operating conditions.
If thermal validation is required, the applicable test or acceptance requirements should be agreed for the specific project.
MOQ and estimated lead time depend on tooling availability, profile complexity, quantity, finishing, machining and whether new tooling and trial samples are required.
They are confirmed after technical review rather than published as fixed values for all power heat sinks.
Yes, where the cross-section and application are suitable for extrusion.
The profile may combine external heat-dissipating surfaces with structural walls and internal mounting interfaces.